Hydraulic Cylinder & Industrial Honing Services
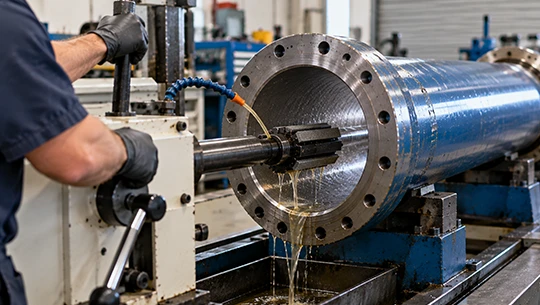
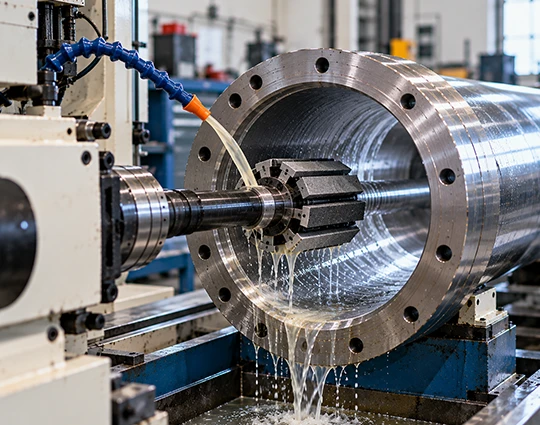
Precision honing is an internal finishing process used to improve the condition, geometry and surface finish of cylindrical bores.
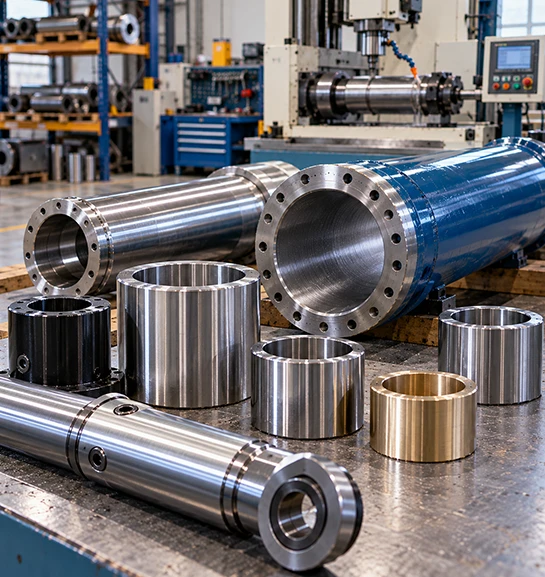
We provide honing services for hydraulic cylinder barrels, cylinder bores, sleeves, bushes and other cylindrical industrial components where accurate internal finishing is important for reliable operation.
Honing can remove suitable surface imperfections, correct minor bore irregularities and produce the required internal surface finish for the component application.
With honing capability for components up to 8 metres in length and bore diameters up to 12 inches, we support hydraulic and industrial honing requirements across Sydney, NSW and Australia.
What Is Precision Honing?
Precision honing is an abrasive machining process used to finish the internal surface of a cylindrical bore.
The process removes a controlled amount of material to improve the bore’s geometry, dimensions and surface finish.
For hydraulic cylinders, the condition of the internal bore is important for piston movement, lubrication and seal performance. Where the existing bore is suitable for honing, the process can improve the internal surface without requiring replacement of the complete component.
What Components Can Be Honed?
Honing is commonly used for cylindrical components where the internal bore requires controlled finishing, restoration or dimensional correction.
Our honing services are suitable for:
- Hydraulic cylinder barrels
- Hydraulic cylinder bores
- Sleeves
- Bushes
- Cylindrical industrial components
- Engineered components requiring internal surface finishing
The appropriate honing approach depends on the component dimensions, material, existing condition and required final specifications.
Hydraulic Cylinder Honing for Bore Restoration
The internal bore of a hydraulic cylinder plays an important role in piston movement, lubrication and seal operation.
Continuous use can result in scoring, wear, corrosion marks and other surface imperfections inside the cylinder barrel.
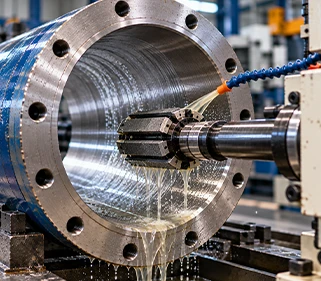
Hydraulic cylinder honing can restore the internal surface of a suitable bore by removing controlled amounts of material and improving the bore finish.
For complete hydraulic cylinder restoration, honing can form part of our broader hydraulic cylinder repair service.
Improved bore surface condition
More consistent internal dimensions
Better conditions for seal operation
Improved lubrication
Reduced friction
Improved surface finish
Hydraulic Cylinder Bore Honing & Internal Surface Finishing
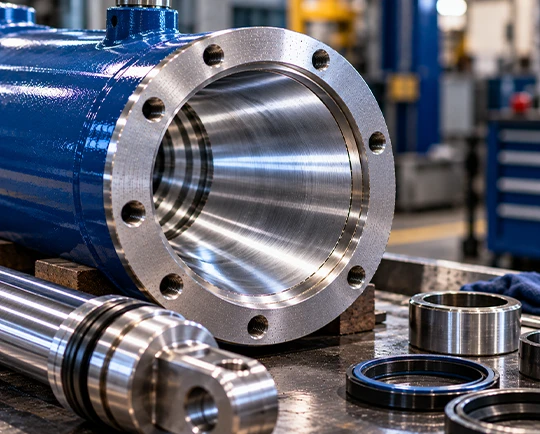
Honing is particularly useful when the internal surface of a cylinder bore requires controlled finishing after wear or surface damage.
Depending on the condition of the component, honing may be used to address:
- Internal scoring
- Surface wear
- Minor corrosion marks
- Bore irregularities
- Surface imperfections
- Conditions affecting seal operation
The amount of material removed depends on the existing bore condition and the required finished dimensions.
Where damage is beyond what honing can correct, the component can be assessed for an alternative restoration process.
When Does a Hydraulic Cylinder Bore Need Honing?
Honing may be required when the internal bore condition begins to affect cylinder operation, sealing or component performance.
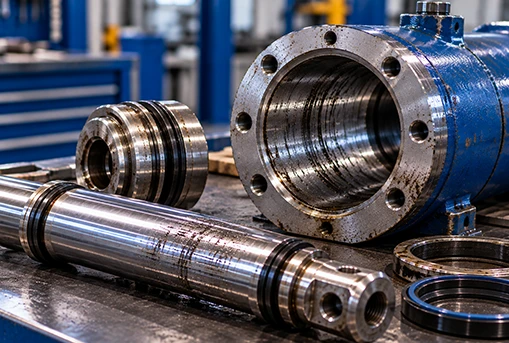
Scoring & Surface Damage
Repeated piston movement can cause scoring and surface imperfections inside a hydraulic cylinder bore. Where the damage is suitable for honing, controlled material removal can improve the internal surface.
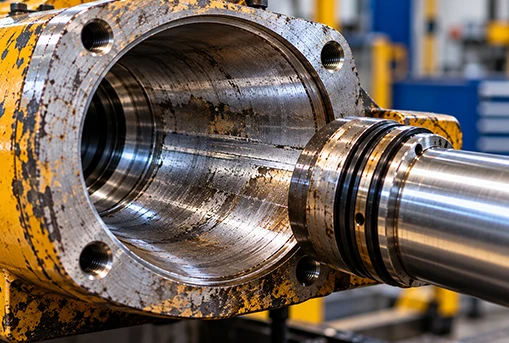
Bore Wear
Long-term operation can cause wear within the cylinder bore. Honing can help restore suitable bore dimensions and surface condition where sufficient material remains.
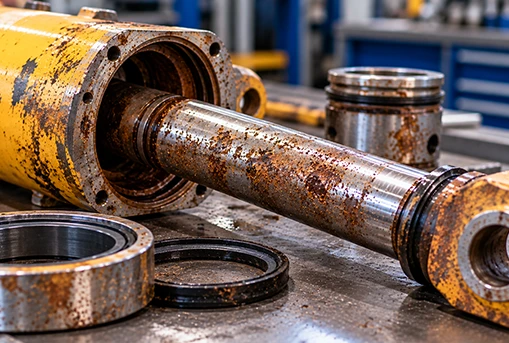
Corrosion & Surface Marks
Corrosion can affect the internal surface of a cylinder barrel. Depending on the severity, honing may be suitable for removing surface marks and restoring the bore finish.
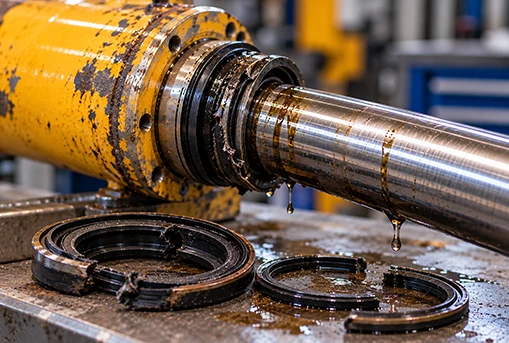
Seal Wear & Leakage
An unsuitable bore surface can contribute to seal wear and leakage. Improving the bore surface can provide better conditions for hydraulic seals to operate.
Our Hydraulic Cylinder Honing Process
A consistent honing result starts with understanding the existing condition of the bore and the required finished dimensions.
01
Bore Inspection
The cylinder barrel or component is assessed to determine the bore condition, dimensions and extent of wear or surface damage.
02
Component Preparation
The component is prepared and positioned for honing according to its dimensions, condition and required finished specifications.
03
Controlled Honing
The internal bore is honed using controlled abrasive action to remove suitable surface imperfections and improve bore geometry and surface finish.
04
Final Inspection
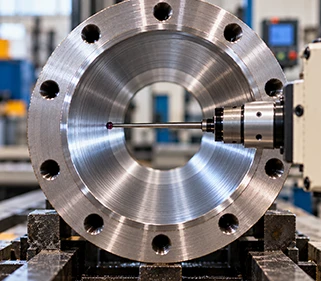
The finished bore is checked against the required dimensions and surface requirements before the component proceeds to assembly or further restoration.
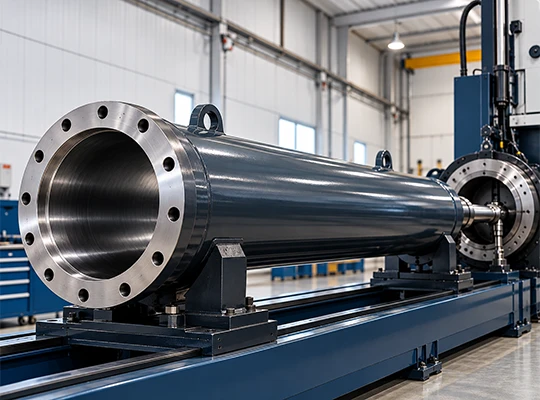
Honing Capability Up to 8 Metres
Our honing capability supports components up to 8 metres in length and bore diameters up to 12 inches.
This allows us to assess larger hydraulic cylinder barrels and industrial components requiring internal bore finishing and restoration.
Component dimensions and requirements can be reviewed before work begins to confirm suitability for the available honing capability.
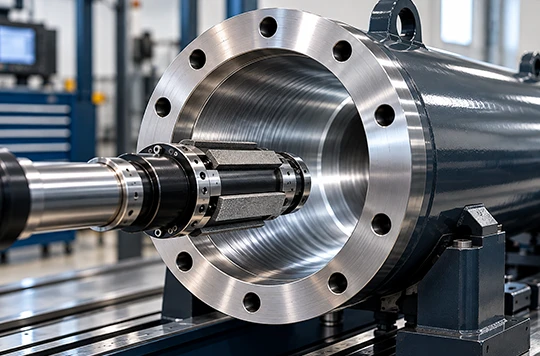
Accurate Bore Dimensions & Surface Finish
Honing can improve bore surface condition, geometry, dimensional consistency and internal surface finish. The resulting bore can provide the required component fit and operating characteristics, depending on the material, existing condition and final application.
Precision Honing for Industrial Applications
Mining & resources
Construction & earthmoving
Manufacturing
Heavy equipment
Industrial machinery
Material handling
Agriculture
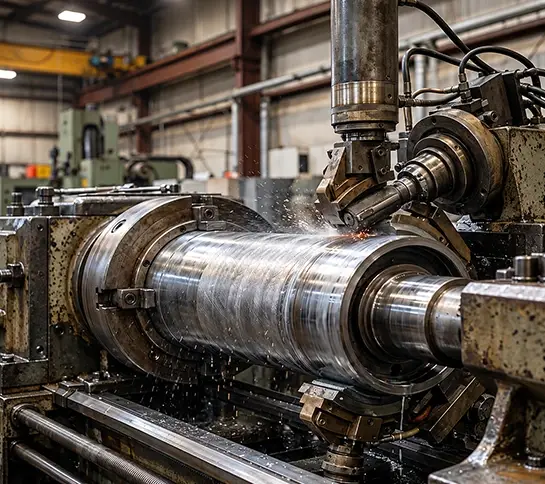
Honing as Part of Component Restoration
Honing can form one stage of a broader component restoration process.
Depending on the condition and requirements of the component, honing may be combined with machining, CNC precision grinding, hard chrome plating or HVOF coating.
The appropriate process sequence depends on the component condition, required dimensions and final application.
For complete hydraulic cylinder restoration, see our hydraulic cylinder repair service.
Precision Honing for Hydraulic & Industrial Components
Large Honing Capability
We can assess components requiring honing up to 8 metres in length and 12 inches in bore diameter.
Hydraulic Cylinder Honing
Our honing service supports hydraulic cylinder barrels where bore condition, surface finish and reliable seal operation are important.
Internal Bore Finishing
Honing focuses on improving the internal condition, geometry and surface finish of suitable cylindrical components.
Engineering Support
Our broader engineering capabilities allow honing requirements to be considered as part of the component's overall restoration process.
Precision Honing FAQs
01. What is precision honing?
Precision honing is an internal finishing process that removes controlled amounts of material from a cylindrical bore to improve its geometry, dimensions and surface finish.
02. What is hydraulic cylinder honing used for?
Hydraulic cylinder honing is used to improve the internal bore condition of a cylinder barrel where wear, scoring, surface imperfections or dimensional changes affect the required performance.
03. Can you hone hydraulic cylinder barrels?
Yes. Hydraulic cylinder barrels can be assessed for honing where the internal bore requires surface restoration, dimensional correction or improved finishing.
04. Can honing remove scoring from a hydraulic cylinder bore?
Suitable levels of scoring and surface damage can be addressed through honing, depending on the depth of the damage and the remaining required bore dimensions. More severe damage may require another restoration process.
05. Does honing improve hydraulic cylinder seal performance?
A correctly finished bore provides an appropriate surface for hydraulic seals to operate against. Honing can improve the bore surface condition where the existing bore condition is contributing to seal-related problems.
06. What is the maximum length you can hone?
Our current honing capability supports components up to 8 metres in length.
07. What is the maximum bore diameter you can hone?
Our current honing capability supports bore diameters up to 12 inches.
08. Can honing be part of hydraulic cylinder repair?
Yes. Honing can form part of a hydraulic cylinder repair or restoration process when the internal bore requires finishing or restoration.
09. What is the difference between honing and precision grinding?
Honing is primarily used for controlled finishing of internal cylindrical surfaces, while precision grinding can be used to finish and restore suitable external or cylindrical component surfaces. The appropriate process depends on the component and required result.
Need Precision Honing for Your Component?
Send your cylinder or component details, bore dimensions, drawings or photos and our team can assess your honing requirements.
Whether you require hydraulic cylinder honing, bore restoration or precision internal finishing for an industrial component, we can review the component and confirm its suitability for the process.